- EDM & complex processes
Reach the Geometry.
Keep the Route Connected.
Part of Dawnmill’s Integrated Precision Machining Capabilities.
Dawnmill uses wire EDM and sinker EDM where part geometry, access or feature condition makes conventional machining inefficient or impractical.
- Wire EDM
- Sinker EDM
- Complex Profiles
- Datum Coordination
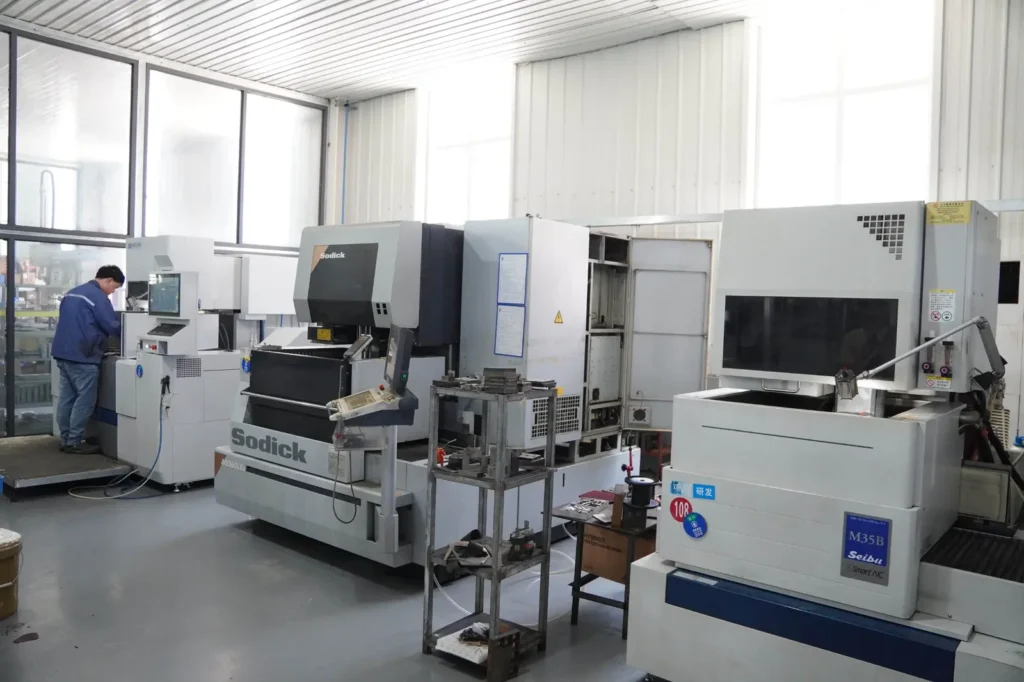
Dawnmill wire EDM workshop · real in-house equipment
- Process applications
Wire or Sinker.
Selected by the Feature.
The geometry determines which process is practical and how it connects with machining and finishing.
Wire EDM
- Precision profiles and cutouts
- Narrow slots
- Controlled through-features
Sinker EDM
- Recessed cavities
- Blind internal features
- Geometry formed by electrode
Combined Machining
- CNC-established datums
- EDM after rough or finish machining
- Secondary features completed in sequence
Final Condition
- Deburring and cleaning
- Specified surface finishing
- Dimensional verification
- Technical specifications & process limits
Define the Range.
Then Commit.
The range below shows what matters for this topic. The applicable process, limits and verification method are confirmed against the actual drawing, material and final condition.
Project-specific values confirmed before production.
Processes In-house wire EDM and die-sinking EDM integrated with CNC-established datums. | Best fit Narrow profiles, controlled through-features, recessed cavities and geometry impractical for rotating tools. |
Materials Electrically conductive materials reviewed against thickness, feature condition and the complete process route. | Control focus Wire/electrode access, stock allowance, datum relationship, corner condition and verification method. |
- EDM review
Use EDM
Where It Earns Its Place.
The process must fit the geometry and the wider route. We review access, stock, datum relationships and the final feature condition before confirming it.
DFM REVIEW
Feature Access
- Whether wire travel, electrode access and surrounding geometry support a practical operation.
- How prior machining leaves stock and establishes datums for the EDM stage.
PROCESS CONTROL
Corner & Surface Requirements
- Feature shape, internal detail and delivered surface condition considered together.
- Machine the references and prepare the required stock condition.
INSPECTION & RECORDS
Datum Relationship
- Keep EDM features tied to the references that define component function.
- Use an appropriate dimensional method for the specified geometry.
PROCESS LOGIC
Machine the Datum. Reach the Feature.
CNC machining and EDM are coordinated so the difficult feature remains connected to the functional geometry of the part.
01
Review Geometry
02
Establish Datums
03
Complete EDM Features
04
Finish & Verify
- Feature control
Difficult to Reach.
Still Clear to Verify.
The inspection approach is considered before the feature is produced, especially where access affects measurement.
REPRESENTATIVE ENGINEERING SCENARIO
Machined body with
narrow EDM slot
Illustrative review scenario—not a published customer case. Customer parts and records remain confidential.
Challenge
A narrow feature must remain related to a machined datum without distorting the surrounding wall.
Process Strategy
Machine the references and stable stock condition first, then complete the EDM feature at the planned stage.
Inspection
Use an appropriate profile or dimensional method tied to the confirmed datum structure.
Result
Target: a controlled wire edm, sinker edm & complex processes route that meets the released drawing and agreed final-condition checks.
CAPABILITY EVIDENCE
Wire EDM and die-sinking EDM performed in-house
EDM planned with CNC machining rather than as an isolated handoff
CMM or optical results, material certificates, FAI and CoC are available when agreed for the project.
- Related Capabilities
Continue Without
Returning to the Menu.
CNC Machining
Establish the main geometry and datum structure before complex features are completed.
Finishing & Secondary Processes
Carry the component from difficult geometry to its specified delivered condition.
Engineering & Quality
Plan access, verification and required records around the feature.
- Questions before the RFQ
Clear the
Important Doubts.
Four topic-specific answers keep the next step practical and direct.
When is EDM preferable to CNC machining?
When feature access, slot width, internal geometry or the required corner condition makes a rotating tool inefficient or impractical.
Is wire EDM outsourced?
No. Wire EDM and die-sinking EDM are part of Dawnmill’s in-house process scope.
How is Wire EDM, Sinker EDM & Complex Processes feasibility confirmed?
We review the actual drawing, overall size, feature access, material, tolerances, finish and inspection method, then confirm the applicable route and limits.
Can this process be connected with other Dawnmill capabilities?
Yes. CNC, EDM, stamping, secondary work, finishing and inspection can be coordinated when the finished component requires a multi-process route.
Cannot Reach It?
Send the geometry. We’ll review whether wire EDM, sinker EDM or a combined route is the practical option.
Factory, equipment and inspection photos show real Dawnmill facilities. AI-generated visuals are used only for confidential component and application concepts tied to Dawnmill’s served industries and available manufacturing processes; they are not customer parts, factory evidence or test records.